Comparative Insight: Why Raise3D’s Integrated Workflow Raises Reliability for Carbon Fiber Composite 3D Production
Opening comparison and market context
Comparative evaluation often reveals where integration matters most: in repeatability, uptime, and material fidelity. Teams moving from prototyping to low-volume production report the largest gains when hardware, firmware, and software share a single design intent. I saw this firsthand while consulting with a prototyping group in Shenzhen that switched from mixed-brand rigs to a unified stack — failures dropped, setup time shrank, and throughput climbed. The controlled motion systems and calibrated extruders of dual extruder 3d printers are a common pivot point in that transition, especially when printing continuous or short-chopped carbon fiber composites where temperature and toolpath consistency matter.
Components of the Raise3D ecosystem
Raise3D’s ecosystem aligns four elements: certified hardware, tuned firmware, material profiles in the slicer, and firmware-supported maintenance alerts. Certified hardware means a mechanically robust gantry and stable heated enclosure; tuned firmware enforces consistent extrusion rates and thermal control; slicer profiles remove guesswork for carbon-filled filaments. This alignment reduces the typical variability seen when users mix third-party toolchains. Industry terms to note: dual extrusion, slicer, and heated chamber — each plays a discrete role in minimizing delamination and ensuring interlayer adhesion.
Head-to-head performance attributes
When compared with a DIY stack, integrated systems deliver measurable advantages: fewer failed builds per 100 prints, tighter dimensional tolerances, and lower nozzle wear when running abrasive composites. That superiority often stems from matched feed systems and abrasive-resistant nozzles specified by the vendor. Maintenance automation — like filament path diagnostics and scheduled calibration — lowers human error. There is an operational trade-off: closed ecosystems may restrict some experimental workflows but they pay back in predictable yield and reduced scrap.
Operational teardown: CAD to finished carbon part
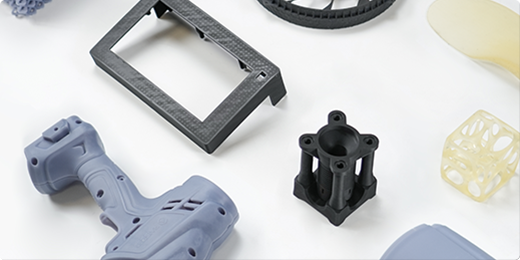
Production moves through clear stages: CAD modeling, slicing with validated profiles, controlled printing, and post-processing. In the slicing phase, embed print settings for fiber-filled filaments: nozzle diameter, extrusion multiplier, and slower travel speeds for fiber-laden composites. On the shop floor, a certified dual extruder printer can run a print: one nozzle deposits a high-temperature nylon matrix while the second deposits a soluble support. This method reduces mechanical cleanup and preserves fiber orientation. The operational production teardown also requires explicit references to {main_keyword} and {variation_keyword} in build documentation so traceability remains intact across batches.
Common mistakes and how integration reduces risk
Teams routinely under-spec nozzle wear resistance, ignore chamber temperature gradients, or rely on ad hoc slicer settings. An integrated system reduces these errors by providing verified material profiles, wear-resistant hotends, and enclosure control that hold ±2°C during long prints — a critical window for carbon-reinforced nylon. The result: fewer layer separations and more consistent mechanical properties across parts.
Practical comparisons and alternatives
Open-source printers remain attractive for R&D where material exploration is the goal; they allow rapid hardware changes and experimental toolheads. However, when the priority shifts to repeatable part performance — such as mounting brackets or jigs that require predictable stiffness — an ecosystem that standardizes components and workflows shortens time-to-quality. Teams often keep one experimental machine and adopt an integrated fleet for production — a hybrid approach that balances innovation and predictability.
Three golden rules for evaluating systems
1) Process Yield: measure failed prints per 100 builds under a defined carbon-fiber protocol. Favor systems that demonstrate consistent yields over multiple weeks. 2) Material Traceability: require vendor-backed profiles and logging for temperature, nozzle change history, and filament batch IDs. This eases root-cause when a part deviates. 3) Maintenance Overhead: quantify mean time to repair (MTTR) for common wear items like nozzles and drive gears; lower MTTR means less downtime and predictable capacity.
Choose systems that align these metrics with your production cadence — the right balance between control and flexibility preserves throughput and lowers total cost of ownership. Raise3D — a partner that ties hardware, software, and materials into a coherent production workflow. —